

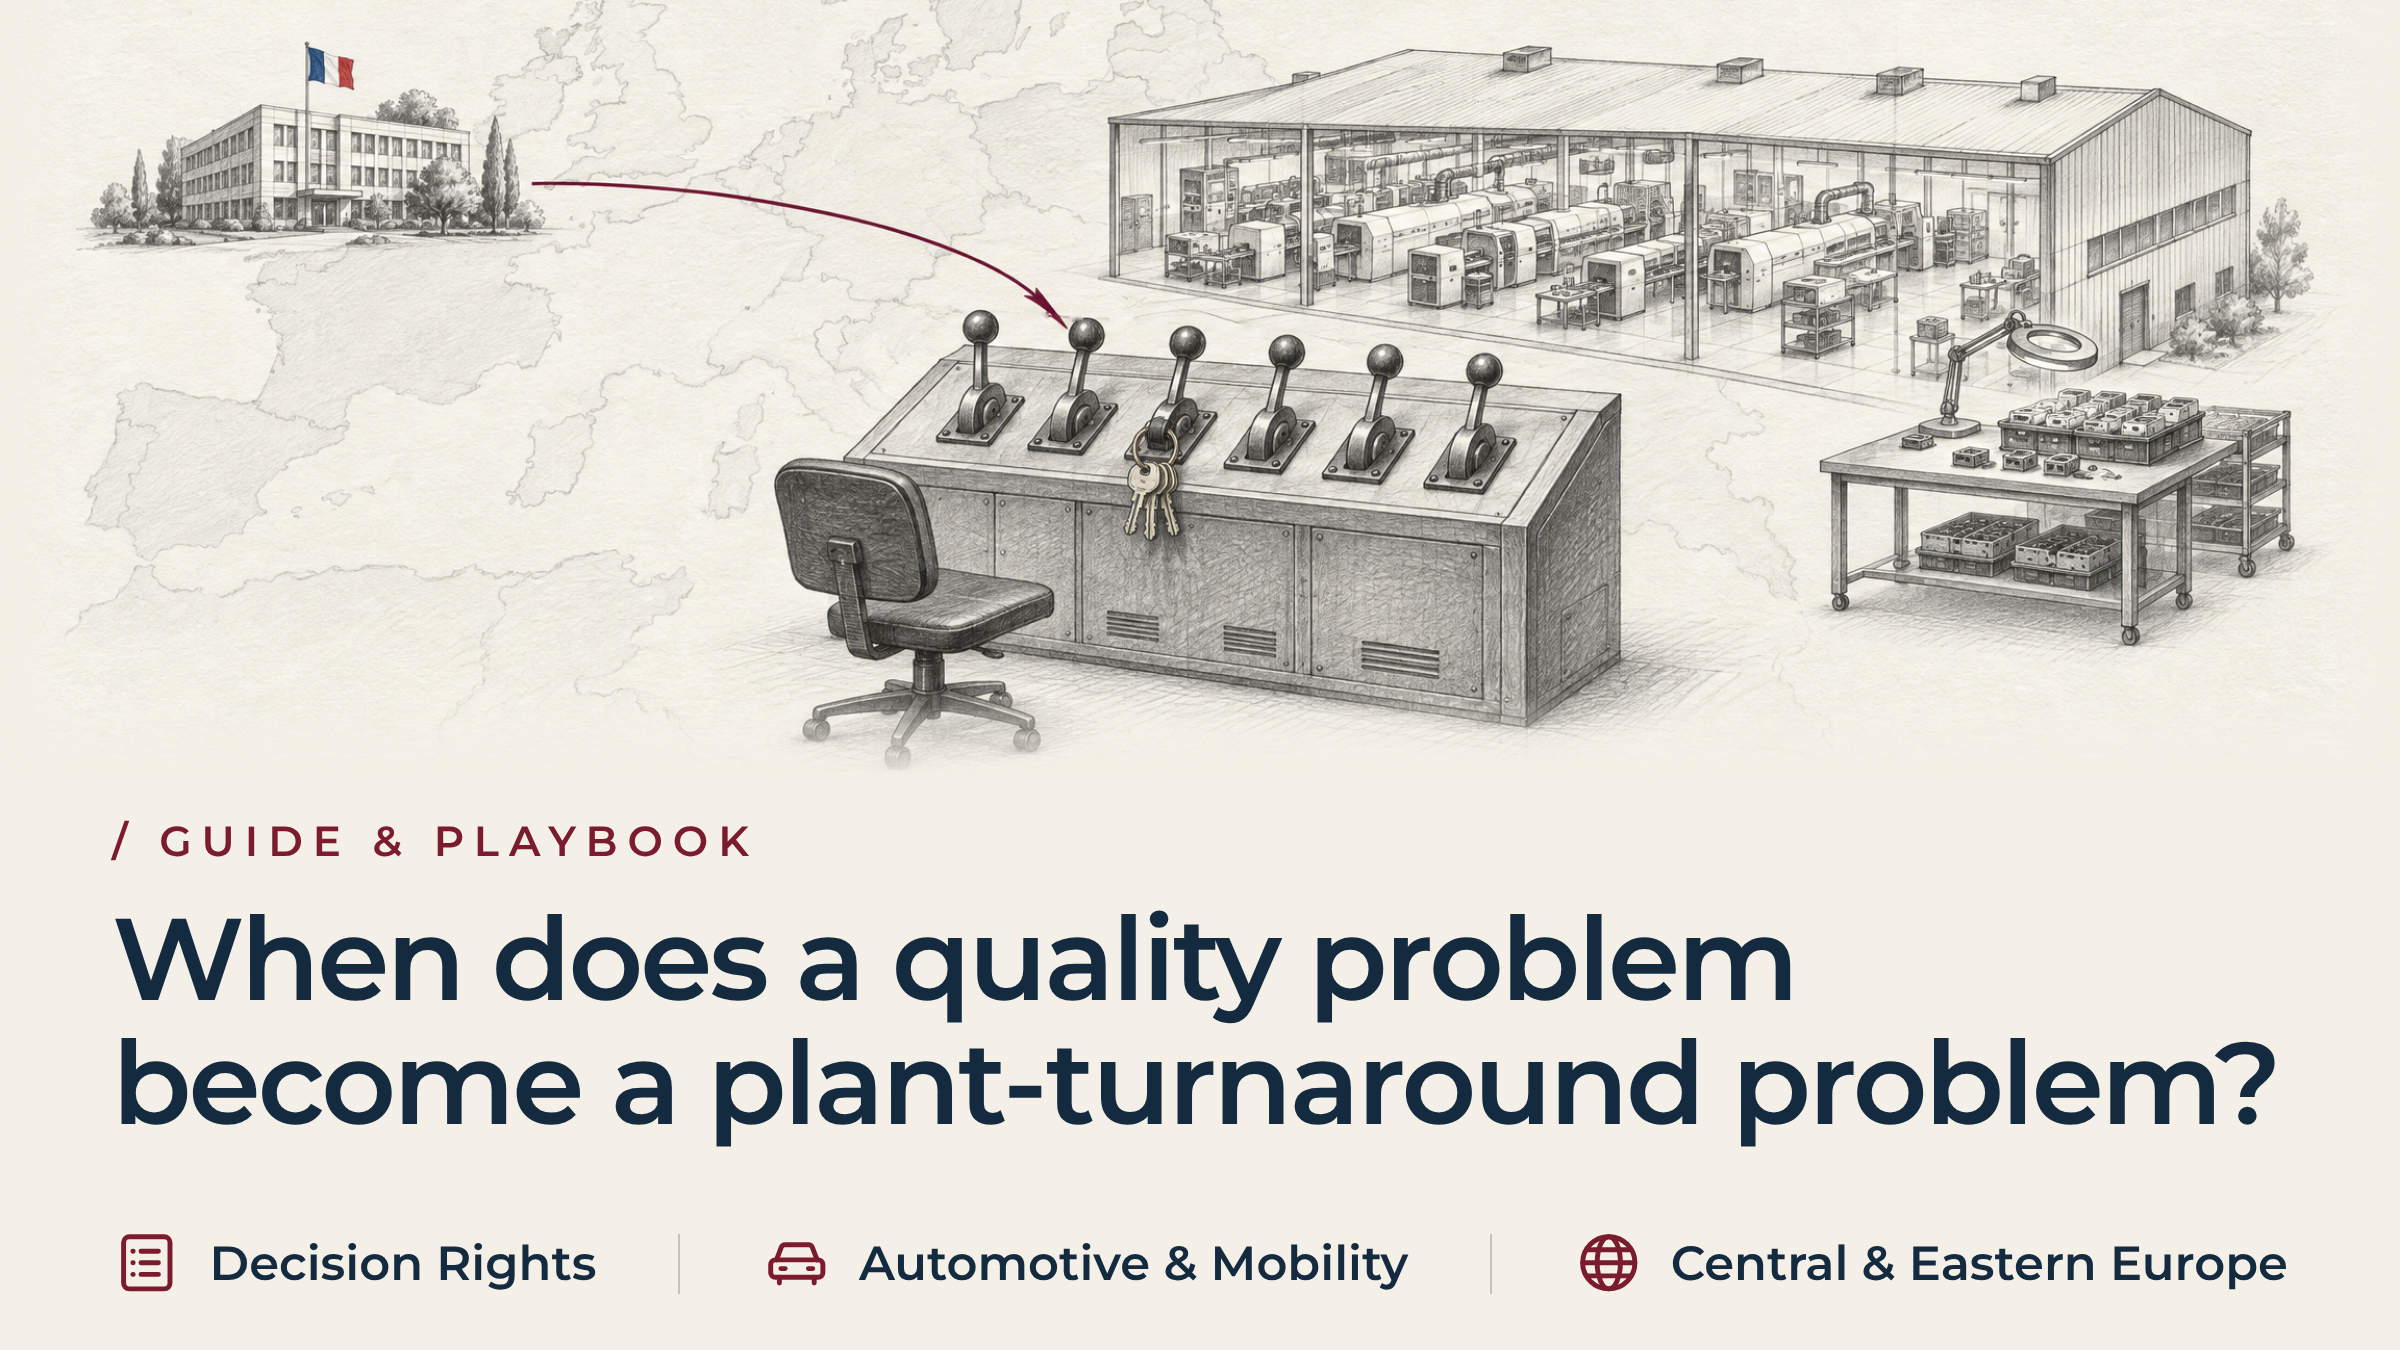
Kdy se problém s kvalitou stane problémem s odstávkou závodu?
Stručně řečeno
There is a recognisable quality problem plant turnaround threshold. It has nothing to do with a scrap percentage. A quality problem becomes a plant-turnaround problem under one condition: the decisions needed to resolve it sit outside the authority of the function that owns the number. Corrective actions run their course, yet the same losses keep recurring. By that point, the plant has usually stopped treating the defect as an exception. The organisation has quietly redesigned production scheduling, maintenance priorities, tooling spend and shift staffing around it. At that point, asking the quality director to fix it again asks too much of one function. The decision now belongs to several.
The Defect That Will Not Leave the Agenda
The monthly operations review follows a familiar pattern. The quality dashboard shows persistent red indicators. First pass yield stays depressed on the primary line. Internal scrap cost sits above budget. The customer complaint log records the same dimensional non-conformance, month after month.
For several reporting cycles, the quality director has presented a complete corrective action record. The quality team has completed the fishbone diagrams. It has updated the failure mode and effects analyses and added inspection sensors.
The defect still returns. Scrap bins stay full, an offline sorting table stays staffed, and weekend overtime keeps protecting the customer shipment.
At group headquarters, the natural response is to tighten the functional lens. Leaders ask why quality has not enforced the standard. Some consider replacing the quality manager, or sending in a corporate audit. That instinct is reasonable. A red metric with a named owner looks like an accountability gap. Accountability is exactly what a board should check.
The difficulty is that the quality director owns the metric. They rarely own the six levers that produce it. Those levers are maintenance scheduling, tooling refurbishment, raw material specification, line speed, shift staffing and customer release planning.
Holding one functional leader accountable for a system-wide outcome will not correct the defect. It mainly delays the moment someone asks who has the authority to change it.
Why the Boundary Is Harder to See Across Borders
When a group manages plants across several countries, headquarters reads performance through standardised indicators. Parts-per-million defect rates, scrap as a percentage of revenue, and open customer 8D counts all describe the symptom. They say little about what the plant has quietly done to keep shipping around it.
On the factory floor, the commercial consequence of a stopped line is immediate. Suppose a stamping die starts to drift after four hours of continuous use. Supervision rarely halts the press to recondition the tool, because halting it risks a missed dispatch. Temporary operators sort parts by hand instead, deburr edges, and feed marginal components back into secondary fixtures.
That is a sensible short-term answer to an urgent delivery commitment. The difficulty begins once it repeats for long enough to become permanent.
How the Workaround Becomes the Operating Model
A workaround like this usually survives a few operating cycles. Then it stops being an exception and starts appearing inside the plant's own planning documents. Three changes tend to mark that shift.
- Production schedules begin allocating fixed machine hours, headcount and floor space to sorting and rework. This stops treating them as occasional overflow.
- Manufacturing engineering writes standard work instructions for the rectification table. This gives the workaround the same procedural status as the approved process.
- Plant controlling opens an accounting code that absorbs the rework labour into indirect overheads. It stops showing up as a variance against the original process cost.
Once those three changes are in place, acceptable delivery no longer proves the process is stable. It is evidence of a second, unofficial operating model, built to protect the first one's output number. What looks like a single quality failure is really a cross-functional quality failure. It spreads across six operational levers, not one function underperforming.
Recognising the Quality Problem Plant Turnaround Threshold
No fixed percentage, universal escalation rule or typical recovery time can define this moment. Every plant's process and margin profile sits inside its own constraints. A general numerical rule would invent precision rather than diagnose the plant's real position. A consistent set of qualitative signals recurs instead. Four of them matter most.
- Rework has entered standard production planning. The plant formally allocates machine hours, headcount and floor space to sorting. It no longer treats this as an exception to close out.
- The root cause spans more than one function. Resolution needs changes to maintenance intervals, material specification, line cycle times and staffing together. No single functional head has standing to order that across peers.
- Containment is consuming plant bandwidth and working capital. Quarantine areas, offline inspection loops and non-conforming inventory tie up floor space. They also absorb cash the plant needs for its primary output.
- The site cannot remove the defect without triggering a delivery crisis. It cannot schedule tooling repair, a machine overhaul or process redesign without immediately threatening a shipment. That means it has lost its operating buffer.
When these four conditions appear together, managing the issue as a quality problem will not resolve it. The decisions required have already moved beyond the function holding the metric. That is the real test of when quality needs executive authority, rather than another correction cycle, and the clearest practical sign that a quality problem has become a plant-turnaround problem.
Sizing the Mandate to the Decisions, Not the Metric
Recovery depends on matching the size of the executive mandate to the decisions it must cover. The department whose scorecard turned red first should not determine that size.
AIAG's CQI-20 problem solving guideline builds executive support and a cross-functional team into every stage of structured problem solving. It does not treat the work as something the quality function finishes alone. That framing matters. A source outside CE Interim treats chronic non-conformance as a leadership question, not only a quality-department one.
Treating it that way starts with the accounting. The American Society for Quality's established cost of quality framework separates prevention and appraisal spending from the cost of poor quality itself. It gives a plant a transparent reference point rather than a fixed benchmark. Applied to this defect, that includes direct labour, scrapped material, exceptional freight, external sorting, machine downtime and tooling wear.
Viewed as a single line against the plant's own profit and loss account, the case for executive-level authority becomes clear. This accounting step is often what finally makes that threshold visible to a board that has only ever seen the defect in fragments.
Realigning the Incentives That Created the Defect
A mandate sized to the decision also needs standing to change how the organisation measures people. It is not only about what the organisation tells them to do. Three realignments recur often enough to be worth naming.
- When supervisors' targets reward only daily unit output, they will resist the line stoppages a maintenance fix requires. The stoppage counts against their number before the fix shows any benefit.
- When procurement's target rewards only unit cost reduction, it will keep buying marginal inputs that create downstream scrap. The saving is visible, but nobody charges the scrap cost back to procurement.
- When the organisation tells supervisors to protect customer delivery above all else, they keep running unstable equipment. They do not stop it, because stopping it is the one decision they expect to explain first.
A credible mandate has the standing to put process capability and accepted good output ahead of these local incentives. That is precisely the authority the organisation never gave the quality director.
The Cross-Border Dimension in Practice
Exercising this authority across borders needs presence, not a quarterly review from another country. A committee based in Munich, Zurich or Paris can see the aggregated numbers coming out of the plant. From that distance, it cannot tell whether the approved process is protecting the number. An unofficial one running alongside it may be doing the work instead.
A credible intervention starts with direct verification. The executive walks the lines, examines quarantined inventory, and sits in on shift handovers. They talk to the operators, toolmakers and maintenance technicians who already know where the real constraint sits.
It also means protecting the plant from premature interference while the fix is under way. Halting unstable equipment for a tooling overhaul reduces output for a period. The executive needs standing to manage that conversation with customers and with the commercial function at headquarters. A temporary dip should not read as a new crisis.
The board keeps the strategic decisions: site footprint, commercial terms, capital investment. The mandate it grants is for execution. It covers stabilising daily operations, resequencing maintenance and production priorities, and building the local capability that holds the fix in place once the mandate ends.
Case Study: When a Wiring Plant's Quality Crisis Became a Turnaround Mandate
A French Tier 1 automotive electronic sensor and wiring assembly manufacturer operates a production facility in Central Eastern Europe. It had spent four months inside an escalating quality crisis. The site quality director ran a complete sequence of 8D corrective actions.
None of it held. The plant's high-speed automated soldering and potting lines kept generating an 18 per cent internal defect rate. Solder bridging and microscopic seal voids triggered repeated customer quality notifications and put a customer line stoppage within reach.
Corporate leadership in Paris read this, understandably, as a compliance failure. It began preparing to replace the local quality manager. Then it became clear the causes crossed several departments rather than sitting inside one. The group chief executive engaged CE Interim instead.
CE Interim placed a vetted, mandate-matched Interim Operations Turnaround Executive on site within 72 hours of the completed mandate brief. The executive carried a direct board mandate with cross-functional authority over production scheduling, maintenance, tooling engineering and quality together.
What the Audit Found
The executive's first task was not to inspect the solder joints again. It was to walk the line, read the shift logs, and ask why the number had not moved. Three findings explained it between them.
- The quality director owned the failure KPI but had no authority over the production schedule. Supervisors' targets rewarded only daily throughput, so the incentive ran the wrong way: overriding thermal sensor warnings and delaying soldering tip changeovers protected a supervisor's number more than reporting a stoppage did.
- Group purchasing was working to a corporate cost-down target. It had switched to a lower-cost flux supplier without validating it against the high-speed automated lines. Nobody had asked quality to approve that decision.
- The plant had quietly built a shadow operation of thirty temporary agency technicians. They hand-reworked and re-soldered defective sensor housings under magnifying lamps. It added 45,000 euros a week in unbudgeted containment cost that nobody had put in front of the board as a single figure.
What Changed in Seven Weeks
With the mandate sized to the whole system, not to quality alone, the executive made three changes in sequence.
- Halted the unstable automated cells for thirty-six hours. This allowed the team to overhaul the soldering wave pots, recalibrate thermal profiles and restore the originally certified flux specification.
- Replaced gross unit volume targets for shift supervisors with accepted first-pass yield. This removed the incentive to push a defective unit downstream rather than stop the line.
- Phased out the offline rework tables entirely. A non-conforming batch now triggers an immediate cell pause and a supervisor escalation, instead of a quiet hand correction.
Within seven weeks, first pass yield on the automated lines reached 96.5 per cent. Customer quality complaints fell to zero. The plant stood down the agency rework team and removed 1.9 million euros in annualised failure and rework cost. None of that needed a different quality director. It needed authority that reached beyond the quality function, reporting to the chief operating officer, with the standing to halt unstable tooling, resequence maintenance and reset supervisor incentives inside one coordinated mandate.
Frequently Asked Questions About the Quality Problem Plant Turnaround Threshold
What Keeps a Manufacturing Non-Conformance a Quality Problem, Rather Than a Turnaround One?
The classification stays quality while the cause sits inside one function and responsibility is clear. Correction should not require changing the production schedule, tooling budget or staffing plan. Once the fix needs decisions outside quality's authority, the classification should change with it.
What Are the Earliest Signs That a Quality Issue Needs Executive Authority, Rather Than Another Corrective Action Cycle?
Corrective actions that repeat without holding are an early sign. So is overtime that keeps rising while volume stays flat, a permanent offline rework table, and a master production schedule that quietly builds in a scrap allowance.
Does Escalating a Quality Issue to a Turnaround Mandate Mean the Quality Director Failed?
No. A chronic defect usually has causes spread across maintenance, procurement, scheduling and production planning. The function has not failed. The problem has grown larger than the authority attached to it, and that distinction is worth explaining to the quality director directly.
Who Should Hold the Turnaround Mandate Once the Threshold Is Crossed?
An operational executive should hold it: someone with direct decision rights over scheduling, maintenance, tooling investment and staffing. They need to sit high enough in the organisation to act across those functions without seeking a separate approval for each one. That seniority, not a title change for the quality director, is what actually moves a plant past this threshold.
How Long Should the Board Wait Before Escalating?
Two cycles is the limit. If the defect survives both, and overtime or offline sorting is still protecting delivery rather than a stable process, the board should escalate. It should not wait for a third cycle to confirm the pattern.
Aligning Executive Authority With Operational Reality
Leaving a chronic quality failure inside a functional department does not protect the organisation. It tends to produce continued margin erosion and recurring customer escalation. It also leaves a quality director held responsible for decisions the organisation never gave them the authority to make.
Související informace a další postup
The question that matters is not whether the quality department is working hard enough. It is whether the authority already inside the building is large enough for the decisions the problem now requires. Where it is not, a conversation with a Prozatímní partner CE je to rozumný další krok.
Další články na toto téma:
- Dočasný finanční ředitel nebo poradce pro restrukturalizaci: kdo obnoví kontrolu nad peněžními toky v polské továrně v tíživé situaci?
- Proč je hledání stálého vedoucího závodu během probíhajícího turnaroudu příliš pomalé
- Prozatímní ředitel závodu, provozní ředitel nebo generální ředitel: Kdo by měl vést oživení maďarského hospodářství?
CE Interim provides cross-border executive leadership for critical business transformations under operational pressure. Where a European manufacturing operation has crossed the quality problem plant turnaround threshold, CE Interim can help.
 EN
 DE
 FR
 IT
 PL
 RO
 CS
 SK
 HU
 ES
 RU
 AR
 SL